
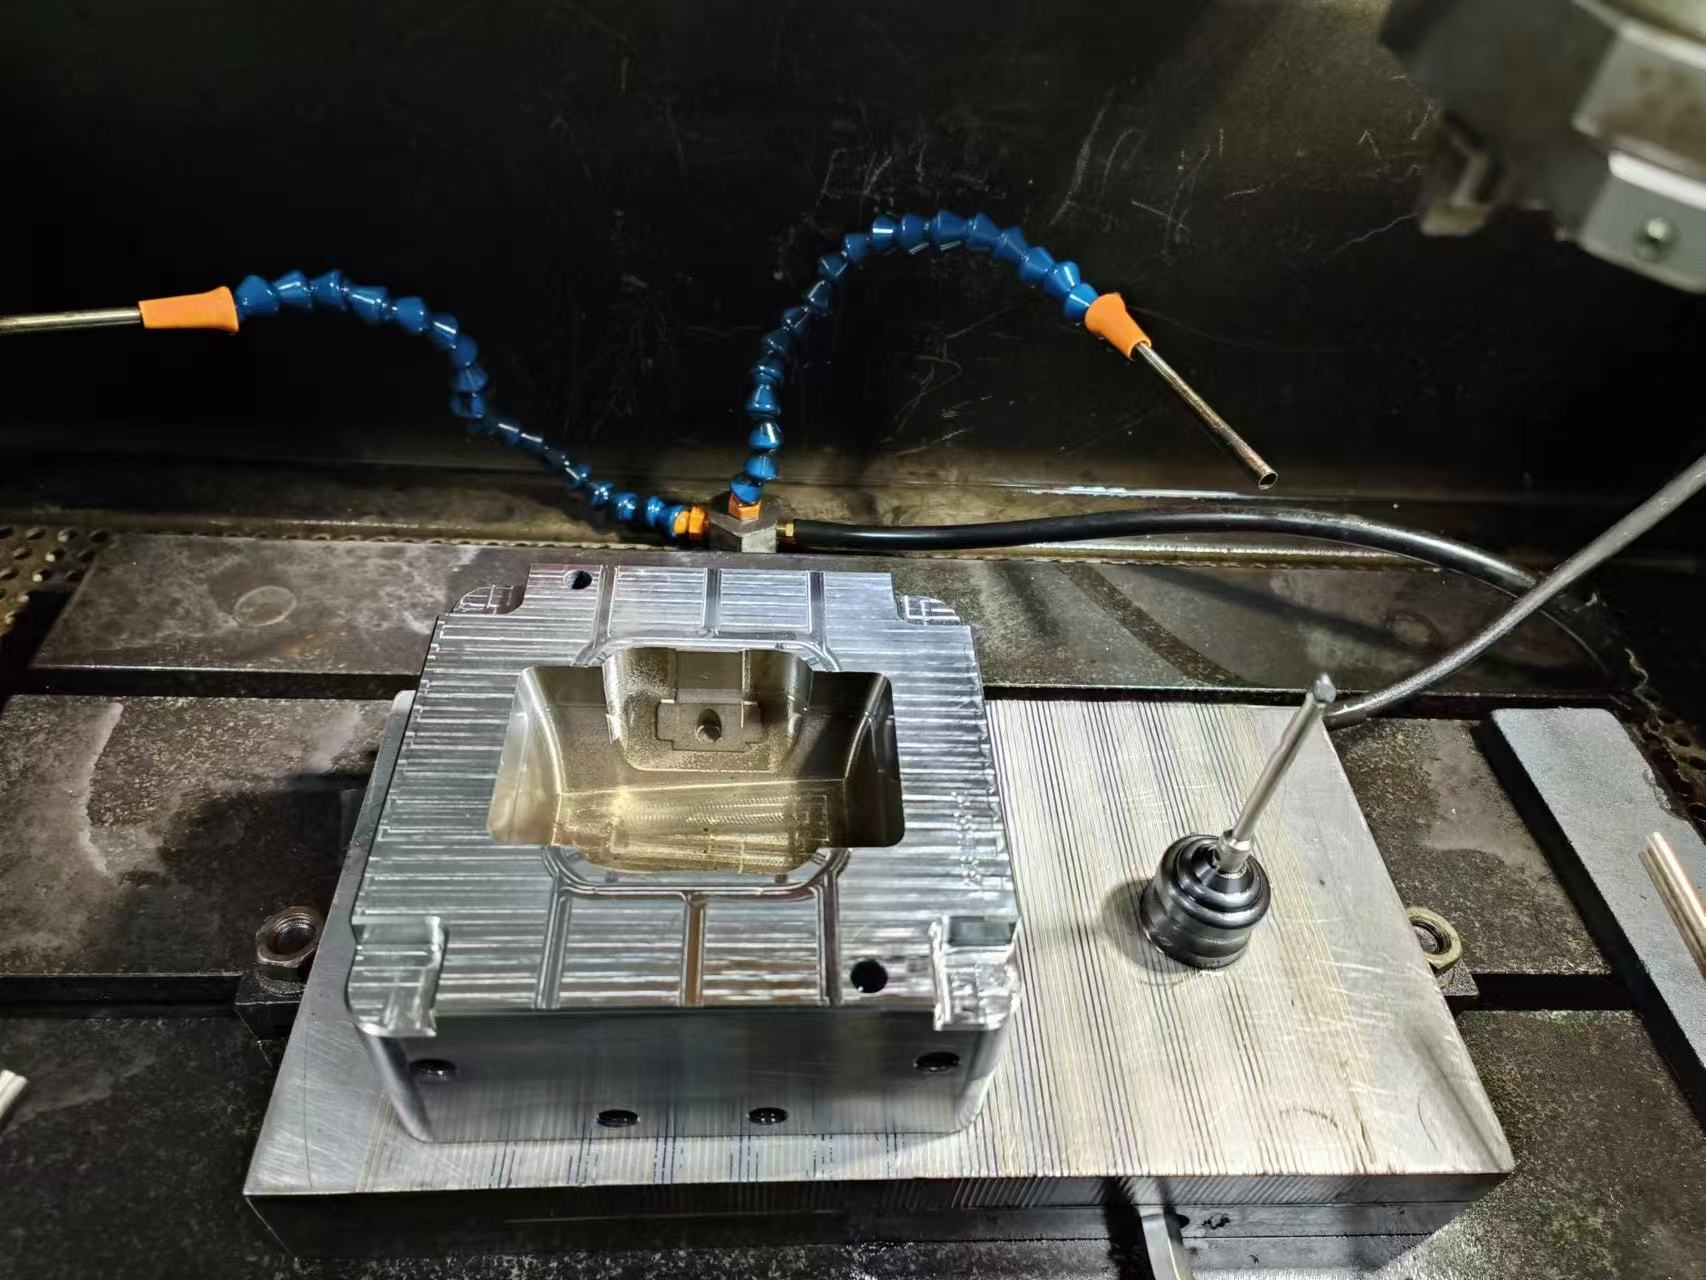
Injection mold repair cost often becomes a problem only after production has already started.
At that point, the buyer wants the mold repaired quickly, while the supplier first wants to know who should pay.
That is where disputes begin.
The best way to avoid this is not to argue after the mold breaks. Instead, both sides should define repair responsibility before production.
A clear agreement should separate normal wear, supplier-related problems, customer-requested changes, and damage caused by incorrect operation.
Why Injection Mold Repair Cost Causes Disputes
A mold is not a maintenance-free tool.
During long-term production, some components will wear.
For example:
- Ejector pins wear
- Springs lose force
- Wear plates become thinner
- O-rings fail
- Sliders develop clearance
- Gates wear
- Small core pins may break
These are normal production issues.
However, other failures may come from poor design, poor steel, bad fitting, or incorrect machining.
The problem is that both situations can look similar after the mold has already failed.
Therefore, buyers and suppliers should agree on the basic rules before mass production begins.
Normal Wear Should Be Defined Clearly
Normal wear is usually the first area that causes disagreement.
A mold may run correctly for a long time, then a wear component needs replacement.
In that case, the repair is usually part of normal maintenance.
Typical wear items include:
- Ejector pins
- Ejector sleeves
- Springs
- Seals
- Wear plates
- Guide bushes
- Small moving components
The exact list depends on the mold structure.
For this reason, the supplier should identify the expected wear parts when the mold is delivered.
This is also why injection mold spare parts are useful for long-term production.
Supplier Responsibility Should Cover Manufacturing Problems
If the mold fails because of a design or manufacturing problem, the situation is different.
For example:
- Steel hardness is incorrect
- A slider locking surface was not designed strongly enough
- Cooling leaks because of poor machining
- A core insert cracks because the steel section is too weak
- Ejector holes are badly aligned
- The mold cannot meet the approved part requirements
These problems are not normal wear.
If the root cause clearly comes from the original mold design or manufacturing, the supplier should normally take responsibility.
However, the key point is evidence.
Both sides should first confirm the root cause before deciding who pays the injection mold repair cost.
Customer Changes Should Normally Be Charged Separately
Not every mold repair is actually a repair.
Sometimes the customer changes the product after the mold is finished.
For example:
- A hole size changes
- A rib is added
- A boss position moves
- A surface texture changes
- A new assembly feature is required
These are engineering changes.
They should normally be treated as mold modifications rather than warranty repairs.
In this case, the supplier should provide a clear quotation before starting the work.
This avoids confusion later.
Operation Damage Is Another Common Dispute
A mold can also fail because of incorrect production or maintenance.
Examples include:
- Closing the mold with foreign material inside
- Running the mold without lubrication
- Using the wrong machine settings
- Running the mold at excessive pressure
- Failing to connect cooling correctly
- Damaging the mold during lifting or transport
If the supplier built the mold correctly but another factory damages it during use, the repair responsibility may not belong to the original moldmaker.
Therefore, operation history matters when evaluating injection mold repair cost.
Injection Mold Repair Cost Should Be Linked to Warranty Terms
A mold warranty should not only state a time period.
It should explain what the supplier actually covers.
For example:
- Mold workmanship defects
- Steel problems
- Machining defects
- Assembly errors
- Cooling leakage
- Early failure of non-wear components
At the same time, the warranty should also state what is excluded.
Typical exclusions may include:
- Normal wear
- Customer modifications
- Incorrect operation
- Accidental damage
- Poor maintenance
- Unauthorized repairs
The clearer the warranty terms are, the easier it is to avoid future arguments.
Do Not Use Shot Count Alone to Decide Responsibility
Shot count is useful, but it does not prove why a mold failed.
A component can fail early because of poor design.
Another component may last far beyond the original target because the mold was maintained well.
Therefore, buyers should not simply say:
“The mold has not reached 500,000 shots, so every repair should be free.”
Likewise, suppliers should not automatically say:
“The mold has already run for months, so every problem is normal wear.”
The actual failure mode should be checked.
A proper injection mold wear inspection can help separate normal wear from abnormal damage.
Root Cause Should Come Before Cost Discussion
This is one of the best ways to avoid disputes.
Before discussing who pays, first identify why the mold failed.
For example:
Case 1: Broken Ejector Pin
Possible causes:
- Normal fatigue
- Bent pin
- Poor alignment
- Part sticking
- Incorrect ejection sequence
The cost responsibility depends on the cause.
Case 2: Slider Damage
Possible causes:
- Normal wear
- Lack of lubrication
- Poor locking design
- Excessive injection pressure
- Incorrect fitting
Again, the failure itself does not tell you who should pay.
The root cause does.
Keep Maintenance Records
Good records make repair discussions much easier.
Useful records include:
- Mold maintenance history
- Shot count
- Repair history
- Part inspection data
- Process settings
- Photos of damage
- Previous mold modifications
For example, if a slider has already been repaired three times in the same area, the history may show that the issue is structural rather than normal wear.
On the other hand, if a wear plate has run hundreds of thousands of cycles before replacement, that may simply be routine maintenance.
This is another reason good injection mold documentation matters.
Injection Mold Repair Cost Should Be Approved Before Work Starts
For non-urgent repairs, the supplier should normally provide:
- Problem description
- Root cause
- Repair method
- Estimated cost
- Lead time
The buyer should approve the repair before the supplier starts.
This is especially important when the repair is chargeable.
Otherwise, the buyer may later say the repair was too expensive, while the supplier may say the work was already completed.
A short written approval avoids this problem.
Emergency Repairs Need a Different Rule
Sometimes production cannot wait.
The mold may stop during an urgent order.
In that case, the buyer may ask the supplier to repair immediately and discuss cost later.
This can work, but both sides should still confirm the basic arrangement in writing.
For example:
- Proceed immediately
- Final responsibility to be confirmed after root-cause review
- Supplier records all repair work and replaced parts
- Buyer receives the final repair report
This keeps production moving without giving up cost control.
Separate Repair Cost From Improvement Cost
Sometimes the mold still works, but the buyer wants better performance.
For example:
- Shorter cycle time
- Better cooling
- Easier ejection
- Improved gate appearance
- More automation
- Better dimensional stability
These changes may improve the mold, but they are not always warranty repairs.
Therefore, buyers should separate:
Repair
from
Improvement
This distinction prevents many unnecessary disputes.
A Simple Responsibility Table
Buyers and suppliers can use a simple rule like this:
| Situation | Typical Responsibility |
|---|---|
| Normal wear | Buyer / production maintenance |
| Original design defect | Supplier |
| Manufacturing defect | Supplier |
| Customer product change | Buyer |
| Incorrect operation | Operator / production factory |
| Accidental damage | Responsible party |
| Warranty workmanship issue | Supplier |
| Performance improvement | Usually buyer |
| Unauthorized third-party modification | Case by case |
This table is not a legal contract.
However, it helps both sides discuss the same categories before production begins.
Injection Mold Repair Cost Is Easier to Control With Spare Parts
Some repair disputes happen simply because the replacement part is not ready.
A small component fails, and the supplier must stop other work to produce it quickly.
That increases cost.
If the mold already has important spare parts, repair becomes simpler.
Typical examples include:
- Ejector pins
- Ejector sleeves
- Springs
- O-rings
- Small core pins
- Wear plates
For export molds, this becomes even more important.
Shipping a small replacement part internationally can take longer than the repair itself.
Buyers Should Confirm Repair Responsibility Before Mold Delivery
Do not wait until the first breakdown.
Before the mold ships, buyers should confirm:
- Warranty period
- Warranty coverage
- Normal wear exclusions
- Spare parts included
- Repair approval process
- Repair labor responsibility
- Shipping cost responsibility
- Third-party repair rules
- Required maintenance records
These points can be included in the purchase order, mold agreement, or final acceptance document.
They do not need complicated legal language.
They only need to be clear.
Final Thoughts
Injection mold repair cost becomes difficult when the responsibility is unclear.
Normal wear, supplier defects, customer modifications, and operation damage should not all be treated the same way.
The best approach is simple:
Define the rules before production.
When a problem occurs, identify the root cause first.
Then decide who should pay based on that cause.
Good maintenance records, clear warranty terms, spare parts, and written repair approval can prevent most disputes.
The goal is not to make every repair free.
The goal is to make repair responsibility predictable before the mold stops production.